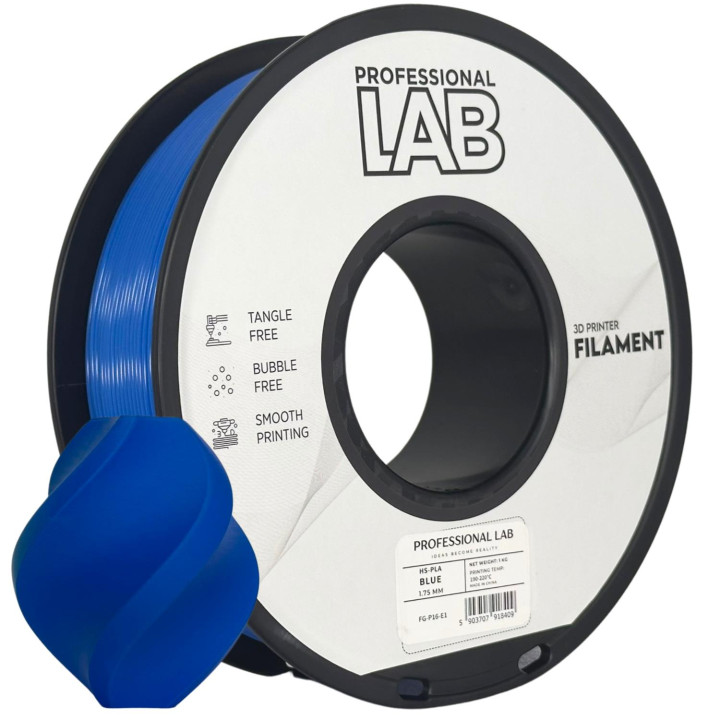
Filament Prof. Lab HS-PLA 1.75mm 1kg | Blue – Optimized for High Speed Printing
Increase the pace of work in your workshop, shorten project implementation time and maintain impeccable geometry precision. Advancedfilament Prof. Lab HS-PLA (High Speed PLA) in an intense, expressive Blue color is a modern premium thermoplastic material. It was created especially for the latest generation of fast 3D printers. The modified rheology of the polymer melt allows for rapid liquefaction of the material in the head and its immediate, stable solidification after leaving the nozzle, which prevents deformations even at extreme feed speeds.
Thanks to the High Speed formula, this material drastically shortens the total printing time, being an unrivaled solution for rapid prototyping, mass production and the creation of conceptual models. The filament is characterized by exemplary layer adhesion, minimal thermal shrinkage and high dimensional accuracy. The intense blue shade is distinguished by uniform pigment saturation along the entire length of the roll and an elegant finish that perfectly highlights construction details. The product is fully compatible with most FDM/FFF 3D printers on the market, unlocking the full potential of machines with increased work dynamics.
Why is it worth choosing High Speed Prof filament? Lab HS-PLA?
- High Speed Optimization: Enables stable operation at very high printing speeds and accelerations, without the risk of underextrusion or loss of structural integrity of the model.
- Rapid prototyping: Noticeably shortens the time spent at the printer, allowing for express testing of subsequent design iterations in the office and laboratory.
- Exceptional ease and fluidity: Maintains the iconic simplicity of use of traditional PLA - it has low shrinkage (low warping), does not require a closed chamber and adheres perfectly to the build platform.
- Rigorous dimensional precision: Control of the 1.75 mm line diameter with a tolerance of up to ±0.03 mm guarantees perfectly even dosing of the material, preventing blocking of the extruder.
Technical parameters and suggested settings:
Filament diameter:
1.75 mm (geometric tolerance: ± 0.03 mm)
Color:
Blue (Blue / Intense)
Plastic type:
HS-PLA (High Speed - polylactide for fast prints)
Net weight of the material:
1.0 kg (gross weight: ~1.3 kg)
Nozzle Temperature (Nozzle):
180°C – 240°C (Higher range values are suggested at maximum speeds)
Table temperature (Bed):
50°C – 60°C (heated bed required)
Spool dimensions:
Outer diameter: 195 mm | Centering hole: 75 mm
Producer / Country of origin:
Imagine s.c., Cholerzyn (Poland)
Compatibility with 3D printers:
The material has been optimized for the increased volumetric flow rate required by modern CoreXY and Delta kinematics.
Perfectly works with ultra-fast devices:
• Bambu Lab (X1 Carbon, P1P, P1S, A1 series) • Creality (K1 series, K1 Max, K1 SE, Ender 3 V3) • Prusa (MK4 with Input Shaping firmware, XL) • Qidi Tech • Voron • RatRig and any other modified machines using Input Shaping algorithms and extruders with high polymer melting efficiency.
Packaging information and operating instructions:
The filament is wound on a stiff spool in a completely orderly manner, which eliminates the risk of the line getting stuck during intensive operation of the extruder. Each spool is factory-packed and hermetically packed in a barrier foil in a vacuum cover with a moisture absorber (silica gel).
Operating tip: Printing at extreme speeds shortens the residence time of the material in the heating block. When setting maximum speed limits in the slicer, it is recommended to raise the nozzle temperature towards the upper limit (230°C - 240°C) to ensure complete and even plasticization of the composite. Before starting work, thoroughly degrease the work table with isopropyl alcohol (IPA). After opening, it is recommended to store the spool in a dry environment with absorbent to prevent hygroscopic flossing.

Comments (0)
Your review appreciation cannot be sent
Report comment
Report sent
Your report cannot be sent